High-Purity Aluminum Powder is chosen not for a label alone, but for the control it can bring to demanding manufacturing processes. When chemistry is consistent, producers can better predict how powder behaves during handling, blending, and consolidation. Particle size, shape, surface condition, and storage history matter too. Purity is only one part of the specification. A certificate may look reassuring, yet buyers still need test methods, batch traceability, and data that match the intended application.
Materials scientist John S. Scully’s published work on materials performance offers a useful reminder: composition and processing conditions both influence results. I cannot verify a direct quotation from him about aluminum powder, so I won’t present invented words as his. A concise guiding line for this article is: “Purity matters when it delivers measurable consistency.” That is an editorial summary, not a quotation.
The practical case becomes clear at the production line. A controlled powder can help reduce unwanted variation, support repeatable feed behavior, and make quality checks more meaningful. Still, higher purity does not automatically mean better performance. Some applications require specific alloying elements or surface characteristics. Others may gain little from paying for a tighter purity grade. The details deserve scrutiny. This guide explains where High-Purity Aluminum Powder can offer real value, what specifications to examine, and which trade-offs buyers should question before selecting a grade. Just a reminder: a small number on a datasheet cannot replace application testing.
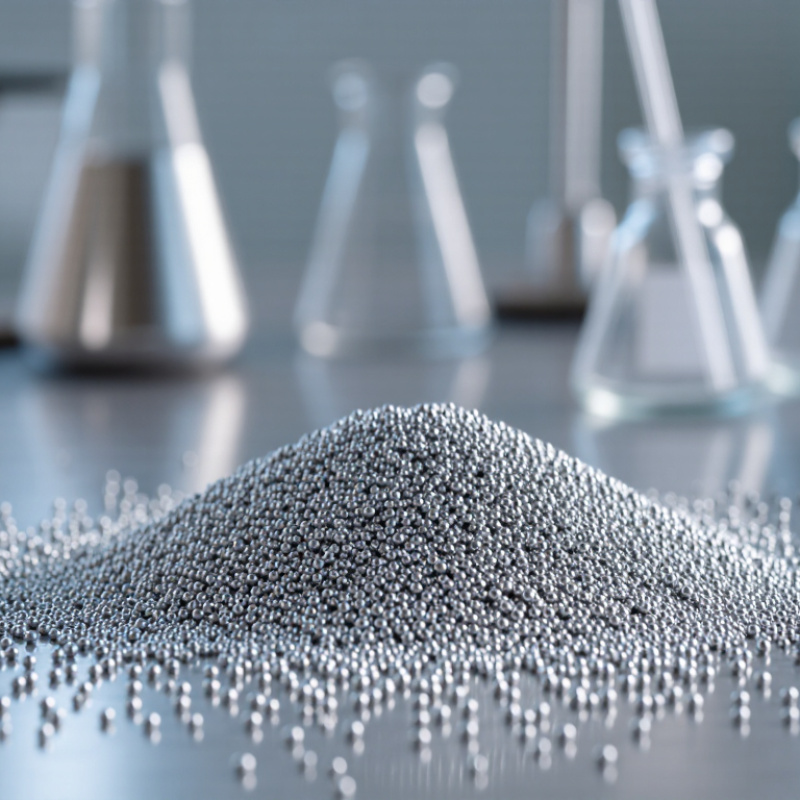
High-purity aluminum powder is finely divided aluminum with a tightly controlled level of metallic purity. The exact threshold varies by grade and application, so read purity claims alongside test methods and impurity limits. Iron, silicon, and copper are commonly monitored. Particle size, shape, and surface condition affect flow, packing, and reactivity. Small details matter.
Production generally begins with refined aluminum melted in a controlled furnace. A stream of molten metal is broken into droplets through atomization, often with gas or water. Gas atomization can produce spherical particles and reduce contamination. The droplets cool, solidify, and are collected as powder. Screening separates size fractions, while laboratory analysis checks composition and particle distribution. Some grades receive surface treatment to limit oxidation during storage. No process makes every particle identical. Sampling can also affect reported results, so certificates should identify the test method and batch.
Tips: Request a batch-specific certificate showing purity and particle-size range. Keep powder sealed, dry, and away from ignition sources; fine metal dust can burn rapidly. If the data sheet is unclear, ask for clarification before selecting a grade.
High-purity aluminum powder contains less non-aluminum material by mass. The chart shows the theoretical total impurity level corresponding to each stated purity, calculated as the remainder to 100% and expressed in parts per million by mass (ppmw). It is illustrative, not a set of product measurements. High-purity aluminum is converted into powder by processes such as atomization; careful control of feedstock and processing helps limit contamination.
Why Choose High Purity Aluminum Powder?
How Its Purity and Particle Properties Are Measured
High purity is not just a label; it is a measured composition. A representative sample may be analyzed by ICP-OES or ICP-MS for metallic trace elements. Oxygen and some nonmetallic impurities often require separate methods, such as inert-gas fusion. Results should identify the test method, detection limits, and whether purity is measured directly or calculated by difference. Particle size is commonly reported as a distribution, not one neat number. Laser diffraction describes size ranges, while microscopy can reveal flakes, rounded grains, or agglomerates. A sieve check can flag oversized particles. That’s different.
Tips: Compare D10, D50, and D90 values across batches, and ask whether the sample was dispersed before testing. Check the certificate for the sampling date and method. Small details matter.
Powder can segregate in transit, so a jar sampled from the top may not represent the whole batch. Apparent purity may also depend on which impurities the method can detect. If a specification and test method don’t align, request clarification before comparing results. Measurements guide selection, but intended process conditions still matter.
High-purity aluminum powder is distinguished by more than its assay value. Chemical analysis shows the concentration of aluminum and trace elements, while particle-size distribution, shape, and surface oxide affect processing. NIST reference data list aluminum’s density at about 2.70 g/cm³ and melting point near 660.3°C. These are properties of aluminum itself, not guaranteed powder-bed values.
Important difference.
For powder, fine particles can expose more surface area to air, making oxide condition and storage history relevant. A certificate of analysis helps verify composition, but it cannot describe how powder will flow or pack. ASTM B213 measures flow rate; ASTM B212 measures apparent density. Both help compare batches under defined test conditions. In practice, a powder that pours smoothly from a sample cup may still behave differently in production equipment. That gap deserves attention. Ask suppliers for particle-size data, test methods, and batch-specific results, then validate with the actual process. NIST and ASTM provide useful reference points, but neither replaces application testing.
High-purity aluminum powder is used in powder metallurgy, where carefully controlled particles can be pressed or sintered into lightweight components. Its low density and strong thermal and electrical conductivity make it useful in applications where weight and heat transfer matter. The final properties still depend on the part’s design and processing conditions.
In additive manufacturing, aluminum powder may serve as feedstock for selected metal-printing processes. Particle size, shape, flow, and surface condition affect how evenly powder spreads across a build platform. Small differences matter. High-purity grades are also used in specialized conductive pastes and coatings, though formulation and processing determine their performance. Purity alone is not a guarantee.
Choosing a powder requires checking more than its purity figure. Buyers and engineers should review particle-size distribution, oxygen content, moisture, and trace elements against the intended process. That detail is easy to overlook. Fine aluminum powder also needs careful storage and handling because airborne metal dust can present a fire risk. In practice, matching the powder specification to the equipment and end use is often more useful than choosing the highest purity available.
Choosing a grade starts with the job the powder must perform, not the highest purity number on a data sheet. For conductive parts, purity and oxide content can affect electrical performance. In coatings or additive manufacturing, particle size distribution and shape may matter just as much. Fine, spherical particles can flow differently from irregular particles, changing how evenly they feed through equipment.
Small details matter.
Ask suppliers for a current certificate of analysis, including purity, particle-size range, and test methods. A headline value alone may hide meaningful variation between batches.
Match the grade to your process conditions. Check whether the powder must disperse in a binder, compact under pressure, or maintain consistent flow through a feeder. Moisture, storage time, and handling can also influence performance, so request guidance on packaging and recommended storage.
There is no universally best grade; a finer powder may improve surface finish but create handling challenges.
That trade-off is easy to underestimate.
Compare samples using the actual equipment and operating settings, then record yield, defects, and flow behavior.
Test before scaling.
Specifications narrow the choice, but a small production trial often reveals what a data sheet cannot.
It can be used in powder metallurgy, selected metal-printing processes, conductive pastes, and coatings. The finished result also depends on design and processing.
Aluminum has low density and conducts heat and electricity well. A pressed or sintered part still depends on its design.
No. The right grade depends on the equipment and intended use. A bigger purity number may not improve the final part.
Review particle-size distribution, shape, oxygen content, moisture, and trace elements. Ask for a current certificate of analysis and its test methods. Easy to overlook.
Fine, spherical particles may flow differently from irregular ones. That can change how evenly powder feeds through equipment or spreads across a build platform.
Purity and oxide content can affect electrical performance. Particle size and formulation also matter; purity alone is not a guarantee.
Check the supplier’s packaging and storage guidance. Fine airborne metal dust can present a fire risk, so handling needs care.
Yes. Compare samples using the actual equipment and settings. Record flow, yield, and defects; a small trial may reveal what a data sheet misses. We might still overlook something.
High-Purity Aluminum Powder is aluminum powder made to meet strict limits on impurities, with its composition and particle characteristics controlled for consistent performance. It is produced through specialized powder-making and refining processes, then evaluated for purity, particle size and distribution, shape, surface condition, and other relevant properties. These measurements help confirm that a powder is suitable for its intended role and behaves predictably during processing.
Its high purity, low contamination, and adjustable particle characteristics can support applications that require reliable material performance, including advanced manufacturing, coatings, and other industrial uses. Selecting the right grade means considering the application’s required purity, particle size, handling and processing needs, and performance conditions. Matching these factors helps balance consistency, suitability, and cost while reducing the risk of choosing a powder that does not meet the requirements.


